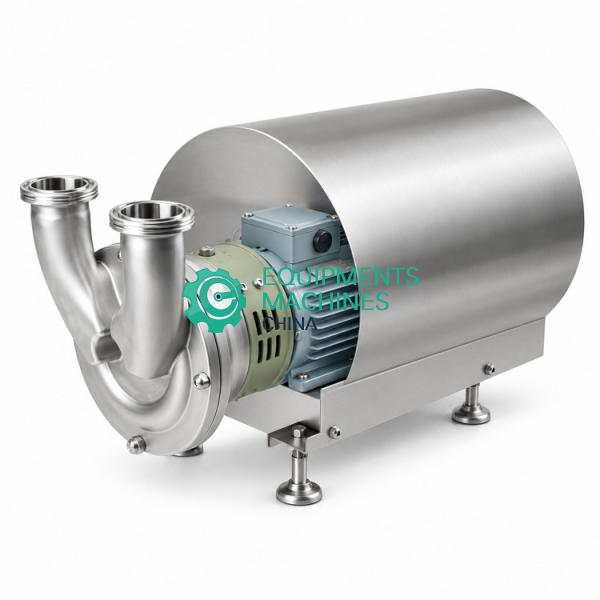
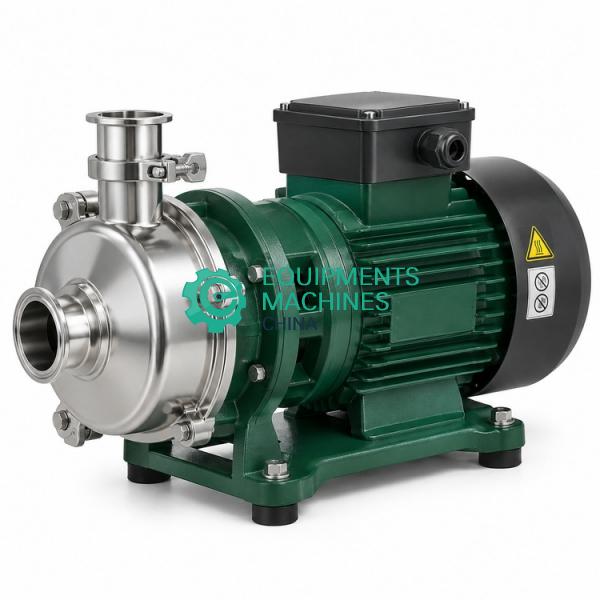
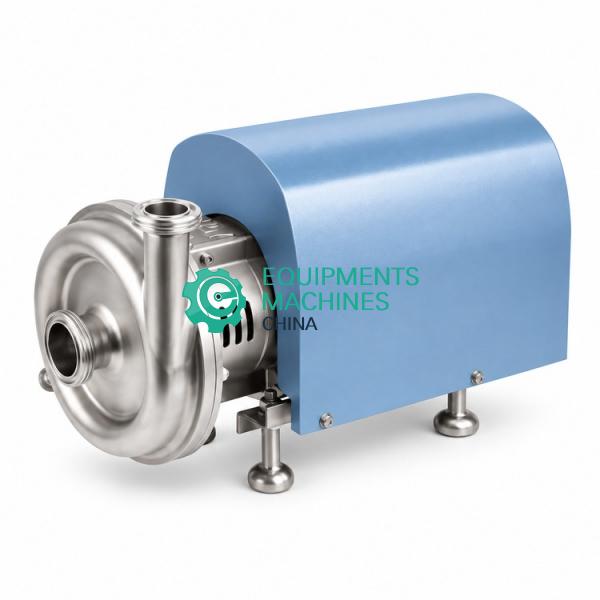
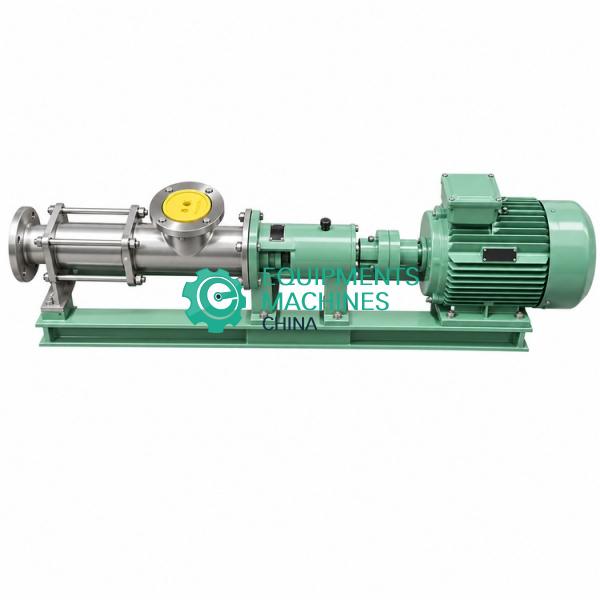
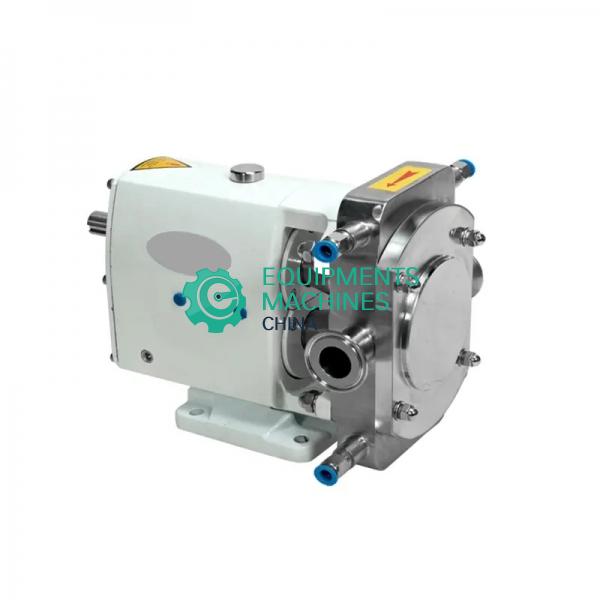
Sanitary Pumps covers hygienic pumping for food, dairy and beverage duty: centrifugal pumps for thin liquids, rotary lobe positive displacement pumps for viscous and delicate product, jacketed lobe pumps for anything that solidifies as it cools, twin screw pumps that handle both product transfer and CIP, and self-priming and liquid ring pumps for return duties. Hygienic design is the defining requirement, meaning surfaces, seals and a geometry that cleans in place without a crevice to trap product.
Positive displacement rather than centrifugal is the choice where the product must not be sheared, which covers yogurt, fruit preparations with particulates, cream, chocolate, fat blends, honey and caramel. A heat jacket extends that to products that set as they cool, keeping them mobile through the pump. Selection comes from the product's viscosity at working temperature together with the flow and discharge pressure, not from the line size alone.
Sanitary pumps are tendered both inside plant packages and separately as replacement and expansion items, through dairy boards and co-operative milk unions, water and beverage authorities, food corporations, breweries, and processing projects under development bank financing. We quote item by item against the specification and provide material certificates where required, hygienic design declarations, performance curves, origin and warranty terms, priced spares and seal kit lists and inspection arrangements.
Tell us your product, its viscosity at working temperature, and your flow and pressure requirement, and we will select the pumps and quote them.